中文简体
 عربى
Content
- 0.1 Introduction to Computerized Flat Knitting Machine Evolution
- 0.2 Carriage System Mechanics and Multi-System Configurations
- 0.3 Needle Bed Architectures: Double-Bed versus Four-Bed Systems
- 0.4 Engineering Analysis of Needle Types: Latch versus Slide Needles
- 0.5 Needle Gauge Mechanics and Fabric Density Optimization
- 1 Technical Specifications and Comparative Systems
- 2 Fabric Manipulation and Take-Down Systems
- 3 CAD/CAM Integration, Programming, and Digital Control
- 4 Operational Troubleshooting and Preventive Maintenance Framework
- 5 Frequently Asked Questions (FAQ)
- 5.1 What is the mechanical advantage of a four-bed computerized flat knitting machine over a standard double-bed configuration?
- 5.2 How does the machine gauge affect the selection of commercial yarns?
- 5.3 What is the specific function of a digital stitch control system in flatbed machinery?
- 5.4 Why are slide needles increasingly preferred over classic latch needles in high-speed machines?
- 5.5 What causes common fabric defects like edge drop-offs and how can they be prevented?
- 6 References and Standards
Introduction to Computerized Flat Knitting Machine Evolution
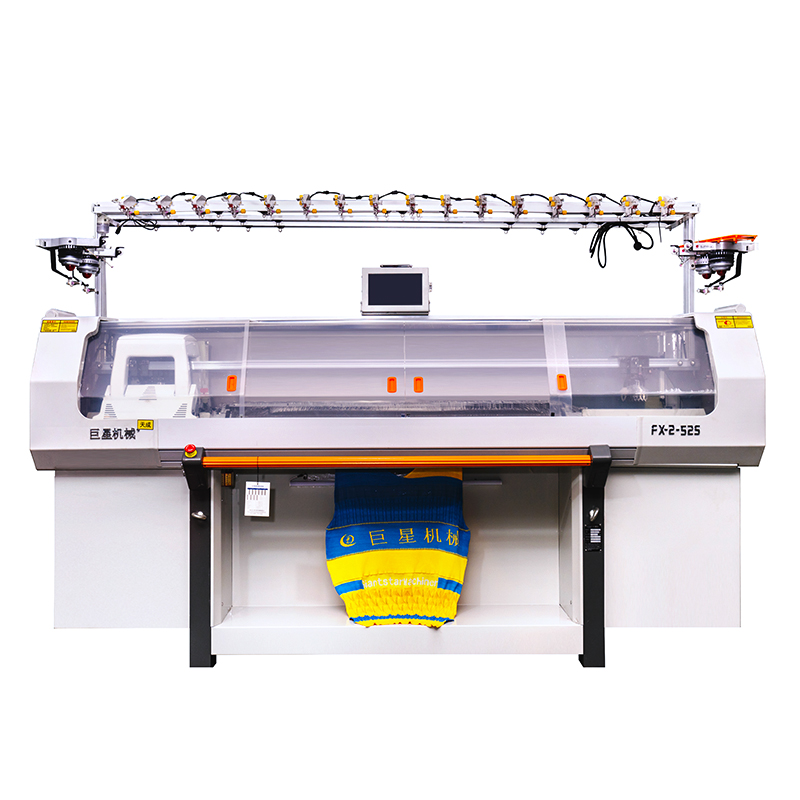
The modern industrial textile manufacturing landscape relies heavily on the capabilities of the computerized flat knitting machine. As a primary piece of weft knitting technology, this machinery has shifted from a mechanically driven needle bed apparatus into a fully automated, digitally controlled manufacturing cell.
At its core, a computerized flat knitting machine utilizes two or more parallel needle beds arranged in an inverted V-configuration, known technically as a V-bed flat knitting system. The machine operates by utilizing a reciprocating carriage that moves laterally across the needle beds, selectively activating individual needles through advanced electromagnetic actuators according to a digital pattern file.
The engineering trajectory of this equipment is defined by the quest for greater geometric design flexibility, accelerated manufacturing speeds, and optimal raw material efficiency. Historically, traditional flat knitting machines required extensive mechanical configurations, including manual cam setups and chain links, to alter stitch styles or garment widths.
The integration of advanced computer numerical control systems, high-speed digital stitch control mechanisms, and programmable yarn carriers has fundamentally transformed the production envelope. Today, the choice of a computerized flat knitting machine directly dictates a factory’s operational capability, determining the complexity of the fabric architectures they can execute, the yarn types they can handle, and the overall throughput efficiency of their production floors. Understanding the deeper structural and operational differences between modern configurations is paramount for commercial procurement teams.
Carriage System Mechanics and Multi-System Configurations
The carriage assembly is the mechanical heart of any computerized flat knitting machine. It houses the complex arrangement of cams, sliders, and electronic selection units that guide the needles through the precise path required for clearing, feeding, knocking over, and loop formation. When evaluating machinery for industrial applications, the number of knitting systems contained within a single carriage is a principal performance metric. A system refers to a complete set of knitting cams that can execute one course of knitting or a loop transfer during a single directional traverse of the carriage.
Industrial configurations typically range from single-system to tandem and multi-system setups, such as double-system, triple-system, or even four-system carriages. A single-system machine can only form one row of loops per carriage pass, making it highly precise but limited in speed. In contrast, a double-system or triple-system carriage can execute two or three independent courses of stitches simultaneously in a single stroke.
This multi-system architecture multiplies the structural output of the machine per cycle. Furthermore, multi-system carriages allow for split functions; for example, in a triple-system machine, the leading system can perform loop transfers from the front to the back bed, the middle system can execute a structural tuck stitch, and the trailing system can knit a plain stitch loop, all within one single movement of the carriage. This concurrency greatly minimizes carriage turnarounds and optimizes cycle times for complex jacquard and structural intarsia patterns.
Needle Bed Architectures: Double-Bed versus Four-Bed Systems
The mechanical configuration of the needle beds determines the dimensional capabilities of the flat knitting machine. The traditional foundational standard is the double-bed computerized flat knitting machine, which features a single front bed and a single back bed. This setup is highly versatile and handles the vast majority of classic knitwear, rib structures, standard links-links patterns, and multi-color jacquards.
However, when advanced shaping, complex three-dimensional geometries, or completely seamless garments are required, double-bed systems encounter spatial limitations because every needle must be carefully shared or left vacant to allow for loop transfers.
To overcome these boundaries, the industry developed the four-bed computerized flat knitting machine. This advanced architecture introduces a pair of auxiliary upper needle beds situated directly above the standard front and back beds, often referred to as top beds or upper beds. The four-bed layout provides a massive expansion in loop manipulation capability.
With four independent beds, the machine can hold loops on the upper beds while the lower beds continue to execute active knitting functions. This eliminates the need for alternate needle techniques—where every second needle must be kept empty to receive a transferred loop—thereby allowing full-gauge fabric production even during highly intricate, fully formed shaping processes. The four-bed structure is the baseline requirement for true whole-garment or seamless manufacturing, allowing the front and back of a garment to be knitted concurrently as an interconnected tube while shaping sleeves and necklines dynamically without structural compromise.
Engineering Analysis of Needle Types: Latch versus Slide Needles
Loop formation inside a computerized flat knitting machine is heavily governed by the specific needle technology embedded within the slots of the needle beds. For decades, the latch needle has been the industry workhorse. The latch needle operates on a simple mechanical principle where a small pivoted latch swings freely to open and close the hook as the needle moves up and down through the old loops and catches the new yarn feed. While highly reliable and cost-effective, latch needles have inherent physics limitations: the mechanical swing of the latch requires a specific physical space, creates high friction at the pivot point at high speeds, and demands a longer stroke distance to fully clear and cast off the loop.
To push past these physical speed limits, modern high-end computerized flat knitting machines frequently employ slide needles, also known as compound needles. The slide needle does not use a swinging latch; instead, it consists of a solid needle body with a flexible hook that is mechanically opened and closed by an independently controlled slider or tongue element running within the same slot.
Because the slider moves in a linear path parallel to the needle hook, the total vertical stroke required by a slide needle is substantially shorter than that of a latch needle. This reduced stroke translates directly into a lower carriage profile, decreased mechanical vibration, and a dramatic increase in maximum carriage travel speeds.
Additionally, slide needles provide superior loop transfer control because the slider tongue can carry and expand the loop with extreme precision, minimizing yarn splitting and breakage when running delicate or high-twist industrial yarns.
Needle Gauge Mechanics and Fabric Density Optimization
The needle gauge, denoted internationally by the letter E followed by a numerical value, is the most defining parameter regarding fabric density, thickness, and yarn compatibility for a computerized flat knitting machine. Technically, gauge refers to the exact number of needles packed into one linear inch of the needle bed. A low gauge number, such as E3, E5, or E7, means fewer needles per inch, wider needle slots, and larger hooks. This configuration is built to handle heavy, coarse yarns like thick wool, blended acrylic cords, and heavy-gauge industrial fibers, producing thick, chunky knit structures.
Conversely, high gauge values like E12, E14, E16, or E18 indicate an extremely dense needle placement with very fine needle profiles and microscopic hooks. These high-gauge machines process ultra-fine yarns, including fine-count combed cotton, delicate mulberry silk, and micro-denier synthetic monofilaments, yielding lightweight, highly compact fabrics with smooth surfaces and excellent drape properties.
Optimizing the interaction between the mechanical machine gauge, the physical yarn count, and the programmable stitch tension is a precise science. If a factory attempts to run a yarn that is too thick through a high-gauge needle bed, the yarn will jam the hook, split the fibers, and cause catastrophic needle damage. Running an excessively thin yarn on a coarse, low-gauge machine results in a structurally unstable, loose fabric with poor elastic recovery.
Modern machines utilize intelligent digital stitch control systems that dynamically adjust the cam down-stroke distance per needle via stepping motors, allowing manufacturers to fine-tune fabric density and achieve uniform loop distribution across the entire width of the fabric panel.
Technical Specifications and Comparative Systems
To assist technical procurement officers and production engineers in evaluating investment choices, the following comprehensive comparison delineates the technical differences across standard commercial configurations of computerized flat knitting machinery.
System Configuration and Bed Architecture Comparison
| Engineering Attribute | Single System V-Bed | Double System V-Bed | Triple System V-Bed | Four-Bed System |
|---|---|---|---|---|
| Active Cams per Carriage Pass | One complete system | Two independent systems | Three independent systems | Multiple lower and upper systems |
| Primary Production Focus | Basic collars, cuffs, simple flat panels | Medium complexity panels, regular jacquard | High speed jacquard, complex intarsia structures | Seamless whole-garment, complex 3D textiles |
| Stitch Transfer Capabilities | Dedicated transfer pass required | Simultaneous knit and transfer operations | Complex multi-stage loop manipulation | Advanced transfer without alternate needle loss |
| Relative Production Speed | Baseline (1.0x) | 1.8x to 2.0x | 2.5x to 2.8x | Optimized for non-stop fully fashioned cycles |
| Yarn Intarsia Flexibility | Limited by carrier paths | Moderate, basic color fields | High, allows rapid carrier changes | Maximum design freedom with independent beds |
| Mechanical Maintenance Profile | Low complexity, minimal cam wear | Standard industrial maintenance cycle | Elevated complexity, precise cam alignment | High technical expertise required for alignment |
Machine Gauge, Yarn Count, and Application Matrix
The relationship between the machine’s physical needle gauge and the appropriate yarn linear mass density is critical to preventing loop deformation and yarn breakage. The following engineering matrix provides standard operating parameters for industrial production planning:
| Machine Gauge (E) | Needles Per Inch | Applicable Yarn Count Range (Nm) | Ideal Cotton Count Range (Ne) | Primary Textile Application |
|---|---|---|---|---|
| E3 | 3 | 1.5 - 3.5 | 0.9 - 2.1 | Heavyweight winter outerwear, chunky blankets |
| E5 | 5 | 3.5 - 7.0 | 2.1 - 4.1 | Coarse knit cardigans, heavy upholstery fabrics |
| E7 | 7 | 7.0 - 12.0 | 4.1 - 7.1 | Standard seasonal knitwear, intermediate collars |
| E12 | 12 | 18.0 - 32.0 | 10.6 - 18.9 | Fine gauge pullovers, lightweight spring garments |
| E14 | 14 | 28.0 - 48.0 | 16.5 - 28.3 | High density activewear components, dress shirts |
| E16 / E18 | 16 - 18 | 48.0 - 80.0 | 28.3 - 47.2 | Ultra fine premium knit garments, base layers |
Fabric Manipulation and Take-Down Systems
Once the needle system creates the loop, the fabric must be systematically drawn away from the active knitting zone to make room for the subsequent course of yarn. This function is managed by the machine’s take-down and sinker systems.
The primary take-down mechanism is located directly beneath the V-bed intersection and consists of a series of segmented, high-friction rollers driven by torque-controlled servo motors. This roller assembly applies a uniform, continuous vertical tension to the knitted fabric, pulling it downwards toward the collection bin.
In modern computerized flat knitting machines, a standard uniform pull-down is often insufficient, especially when knitting fully fashioned or highly asymmetrical three-dimensional panels where some sections have more courses than others. To resolve this, advanced machines integrate an individually controlled auxiliary take-down system or pull-up device. This system features a grid of independent, programmable pins or miniature rollers that apply localized tension exclusively to specific sections of the fabric width.
Complementing the roller system is the spring-loaded moveable sinker system. Positioned at the top of the needle beds, these sinkers hold the fabric loop down horizontally when the needle rises to clear. This action ensures that the old loop remains firmly seated at the base of the needle stem and does not lift up with the needle hook.
The combination of localized take-down rollers and intelligent sinker control allows modern flatbed machinery to execute extreme structural variations—such as pockets, waves, and varying fabric widths—without encountering edge drop-offs, stitch distortion, or structural puckering.
CAD/CAM Integration, Programming, and Digital Control
The operation of a computerized flat knitting machine relies entirely on the translation of creative textile designs into machine readable execution files. This bridge is maintained via dedicated Computer-Aided Design and Computer-Aided Manufacturing software ecosystems. Engineers use these platforms to visually construct the garment profile, define stitch patterns, designate needle layouts, assign yarn carrier paths, and specify carriage speed profiles.
Once the design phase is locked, the CAD software executes a compilation process, converting the graphical stitch map into a sequential array of binary machine commands, often referred to as a knitting program. This program controls every micro-movement of the machine:
- It orchestrates the precise timing of the electromagnetic needle selectors, ensuring that individual needles are raised to the exact required heights (knit, tuck, or miss positions) at carriage speeds exceeding 1.2 meters per second.
- It regulates the electronic yarn feeders, syncing the movement of motor-driven yarn carriers with the carriage path to eliminate slack and ensure correct tension.
- It monitors real-time feedback loops from digital stitch control sensors that measure yarn consumption per course, dynamically adjusting cam pressures to maintain precise, uniform fabric dimensions regardless of slight changes in yarn moisture, room temperature, or batch elasticity.
Operational Troubleshooting and Preventive Maintenance Framework
To ensure maximum machine uptime, prevent structural fabric defects, and prolong the lifespan of the precision needle components within a computerized flat knitting machine, industrial operations must adhere to a strict, structured maintenance schedule. Mechanical wear, lint accumulation, and thermal variance are the primary drivers of processing errors on the factory floor.
Weekly Maintenance Protocol
- Needle Bed Depressurization and De-linting: Use high-pressure compressed air lines to blow out accumulated yarn lint and fiber dust from the needle slots and slider grooves. Built up lint alters needle friction and causes irregular loop heights.
- Actuator and Cam Inspections: Inspect the carriage underside to ensure that the electronic actuators are moving freely and that no wax or yarn finish buildup has settled on the cam surfaces.
- Yarn Tensioner Verification: Clean the top tension disks and lateral yarn guide springs, verifying that the automatic break sensors trip correctly when excessive tension is applied or when a knot is detected.
Monthly Deep Maintenance Protocol
- Needle Channel Lubrication: Apply specialized, low-viscosity, non-staining industrial knitting oils directly to the needle hooks, jacks, and sliders. This must be managed through the machine’s automated lubrication pump configuration, ensuring the volume is calibrated to prevent fabric oil stains.
- Sinker and Take-Down Calibration: Check the wear profile on the moveable sinkers and verify that the rubber coating on the main take-down rollers has not degraded or slicked, which reduces fabric pulling friction.
- Electronic Sensor Self-Tests: Execute diagnostic software routines to check the calibration of the digital stitch control system and verify the positioning accuracy of the carriage encoder strip.
Frequently Asked Questions (FAQ)
What is the mechanical advantage of a four-bed computerized flat knitting machine over a standard double-bed configuration?
A four-bed computerized flat knitting machine features two auxiliary upper beds located directly above the standard front and back beds. This allows the machine to hold loops on the upper beds while the lower beds execute active knitting. The primary advantage is the elimination of alternate needle techniques during complex transfers, allowing the machine to knit high-density, fully structural whole garments or seamless textiles with full needle usage across all beds.
How does the machine gauge affect the selection of commercial yarns?
The machine gauge determines the needle density per linear inch of the bed. Low gauge values (such as E3 to E7) indicate wide needle slots and larger hooks designed for coarse, high-tex yarns like thick wools and heavy acrylic blends. High gauge values (such as E12 to E18) indicate ultra-fine needle profiles engineered exclusively for low-tex, fine count yarns like mulberry silk or fine combed cotton. Mismatching yarn thickness to gauge results in needle breakage or structurally unstable fabric.
What is the specific function of a digital stitch control system in flatbed machinery?
A digital stitch control system acts as a real-time electronic feedback loop during the knitting cycle. It continuously measures the volume of yarn being consumed by the active needles per course. If it detects variation due to yarn tension fluctuations, ambient humidity, or material elasticity, it instantly commands integrated stepping motors to adjust the cam down-stroke depth, ensuring perfect loop uniformity and dimensional stability across all produced fabric lots.
Why are slide needles increasingly preferred over classic latch needles in high-speed machines?
Slide needles utilize an independently controlled linear slider tongue rather than a swinging mechanical latch to seal the needle hook. This reduces the overall physical vertical stroke distance required by the needle to clear and cast off a loop. The shorter stroke allows for a lower carriage profile, minimizes machine vibration, significantly decreases yarn splitting, and enables substantially higher carriage operational speeds.
What causes common fabric defects like edge drop-offs and how can they be prevented?
Edge drop-offs occur when the yarn carrier does not properly feed yarn to the terminal needles at the edge of a panel, or when the take-down tension at the fabric edges is inadequate, causing loops to fail to knock over. This is prevented by adjusting the carriage turnaround safety margin via the CAD program, ensuring the yarn carrier leads the needle selection correctly, and calibrating the spring-loaded moveable sinkers to securely hold the edge loops during the clearing stroke.
References and Standards
- International Organization for Standardization (ISO)
ISO 8116-1: Textile machinery and accessories — Knitting machines — Part 1: Vocabulary and classification systems for weft knitting structures. This international standard provides the exact unified nomenclature for identifying V-bed configurations, carriage cam movements, and needle selection technologies used across global manufacturing plants. - The Textile Institute Textbook Series
Spencer, D. J. (2001). Knitting Technology: A Comprehensive Handbook and Practical Guide (3rd ed.). Woodhead Publishing. This classic reference book provides the core mathematical equations for calculating fabric tightness factors, loop length distributions, and the mechanical physics underlying latch and compound needle actions in flatbed configurations. - Institute of Mechanical Engineers (IMechE)
Research Journal of Textile Engineering and Automation Mechanics, Volume 42, Issue 3. This research compilation covers the kinematic analysis of high-speed carriage reversals and explores the integration of stepping motor control inside advanced multi-system computerized flat knitting machines.